Chinese | English
Mandrel cold push bending machine
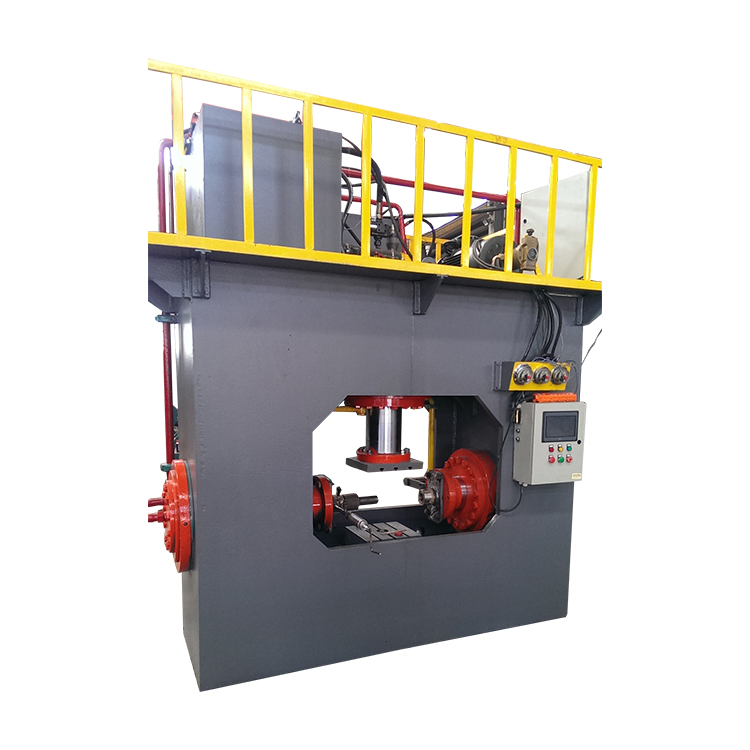
Mechanical parameters
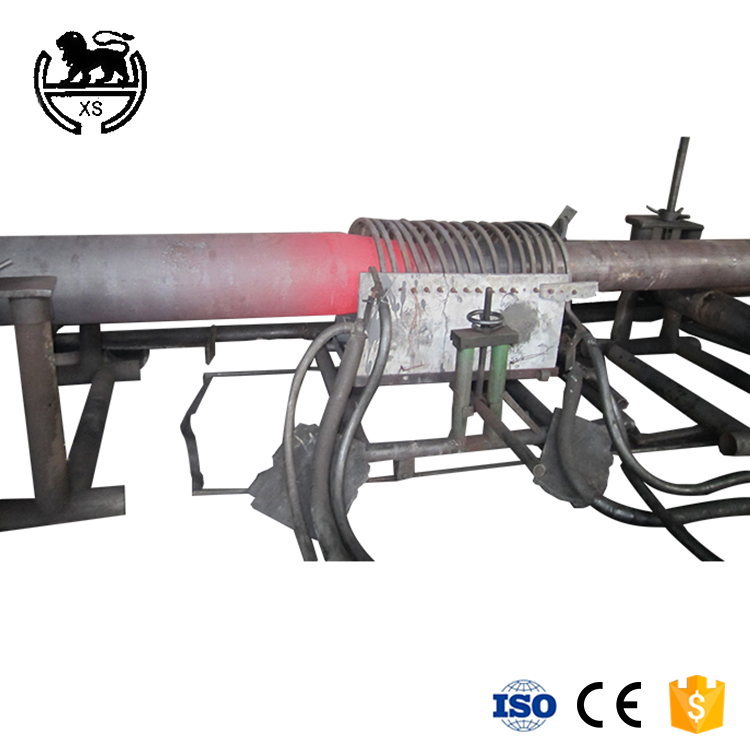
Hot forming elbow machine
|
Processing rangel |
1”—6” |
3”—12” |
8”—24” |
16”—30” |
20”—36” |
30”—48” |
32”—56” |
|
MAX.wall thickness |
Sch40 |
||||||
|
MAX.pressure |
31.5MPa |
||||||
|
Working pressure |
25 MPa |
||||||
|
Working speed |
0—1000mm/min |
||||||
|
Return speeed |
1500—2000mm/min |
||||||
|
Cylinder diameter |
125mm*2 |
180mm*2 |
300mm*2 |
320mm*2 |
360mm*2 |
280mm*4 |
320*4 |
|
Cylinder Stroke |
3000mm |
4000mm |
5000mm |
5000mm |
6000mm |
8000mm |
10000mm |
|
Cylinder thrust |
30T*2 |
30T*2 |
175T*2 |
200T*2 |
250T*2 |
150T*4 |
200T*4 |
|
Motor power |
18.5kw |
22.5kw |
37.5kw |
48kw |
56kw |
68kw |
80kw |
|
IF Power supply needed |
160kwa |
250kwa |
400kwa |
500kwa |
600kwa |
800kwa |
1000kwa |
Mechanical video
Equipment details
- About us ABOUT US Company culture Production ability Service Process Service philosophy
- Device list ELBOW MACHINE PIPE BENDING MACHINE EXPANDING MACHIEN TEE MACHINE BEVELING MACHINE PRESS MACHINE MOULDS
- Video Center ELBOW MACHINE PIPE BENDING MACHINE PIPE EXPANDING MACHINE TEE MACHINE VIDEO BEVELING MACHINE PRESS MACHINE MOULDS VIDEO
- News Center Company news Business news
- Contact us Contact us Web site map
-
