Chinese | English
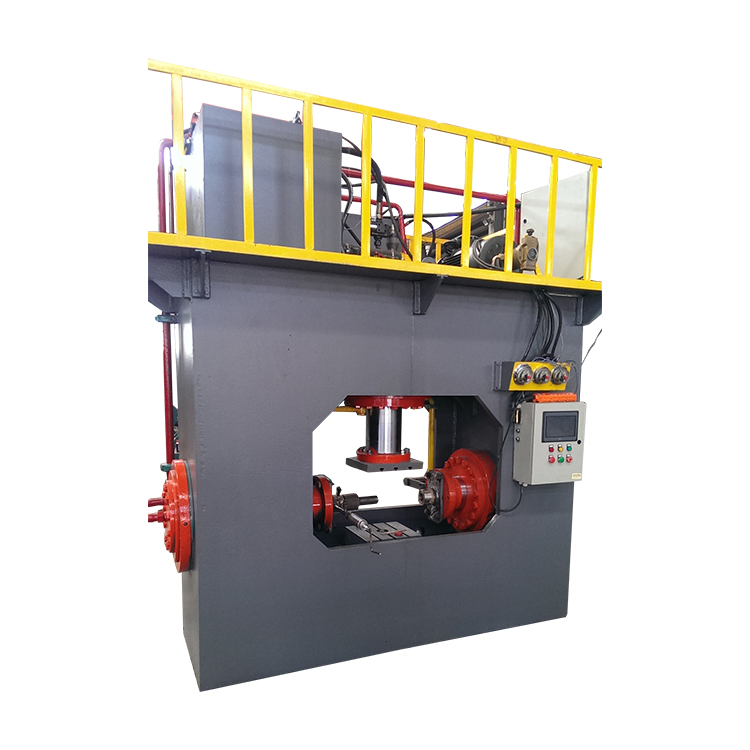
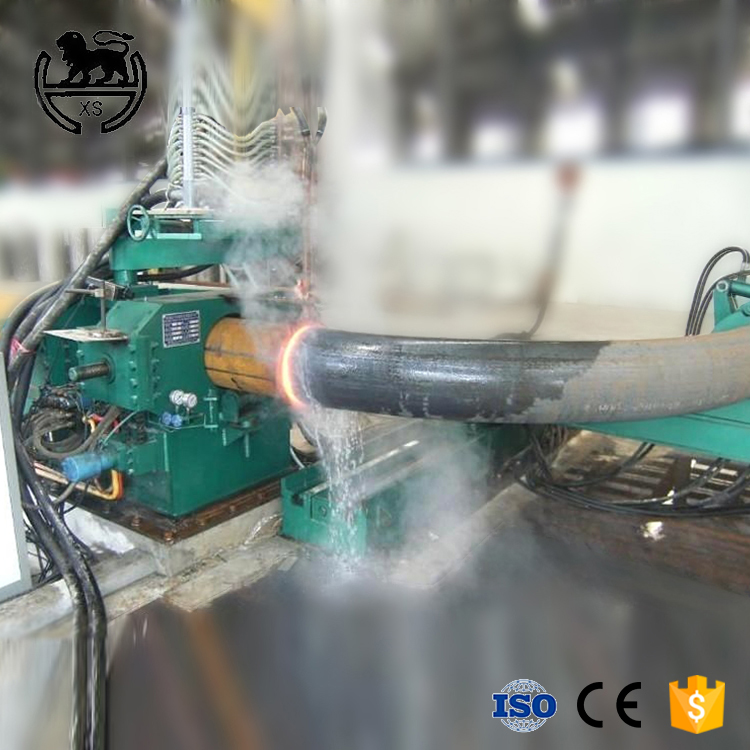
Bulged hydraulic tee machine
Mechanical parameters
Tee machine
|
Processing range |
1/2”—4” |
1”—6” |
2”—8” |
3”—10” |
4”—12” |
5”—16” |
8”—20” |
|
Tee thickness |
Sch40 |
||||||
|
Max.pressure |
31.5MPa |
||||||
|
Working pressure |
25 MPa |
||||||
|
Working speed |
0—1000mm/min |
||||||
|
Return speed |
1500—2000mm/min |
||||||
|
Side cylinder diameter |
360mm*2 |
450mm*2 |
550mm*2 |
650mm*2 |
750mm*2 |
850mm*2 |
950mm*2 |
|
Side cylinder stroke |
300mm |
350mm |
400mm |
450mm |
500mm |
550mm |
600mm |
|
Side cylinder tonnage |
250T*2 |
400T*2 |
600T*2 |
850T*2 |
1100T*2 |
1400T*2 |
1600T*2 |
|
Master cylinder diameter |
400mm |
500mm |
600mm |
700mm |
800mm |
900mm |
1000mm |
|
Master cylinder stroke |
350mm |
400mm |
500mm |
600mm |
700mm |
800mm |
900mm |
|
Master cylinder tonnage |
315T |
500T*2 |
700T |
1000T |
1200T |
1600T |
2000T |
|
The motor power |
50kw |
55kw |
65kw |
75kw |
100kw |
120kw |
170kw |
Mechanical video
Equipment details
- About us ABOUT US Company culture Production ability Service Process Service philosophy
- Device list ELBOW MACHINE PIPE BENDING MACHINE EXPANDING MACHIEN TEE MACHINE BEVELING MACHINE PRESS MACHINE MOULDS
- Video Center ELBOW MACHINE PIPE BENDING MACHINE PIPE EXPANDING MACHINE TEE MACHINE VIDEO BEVELING MACHINE PRESS MACHINE MOULDS VIDEO
- News Center Company news Business news
- Contact us Contact us Web site map
-
