Chinese | English
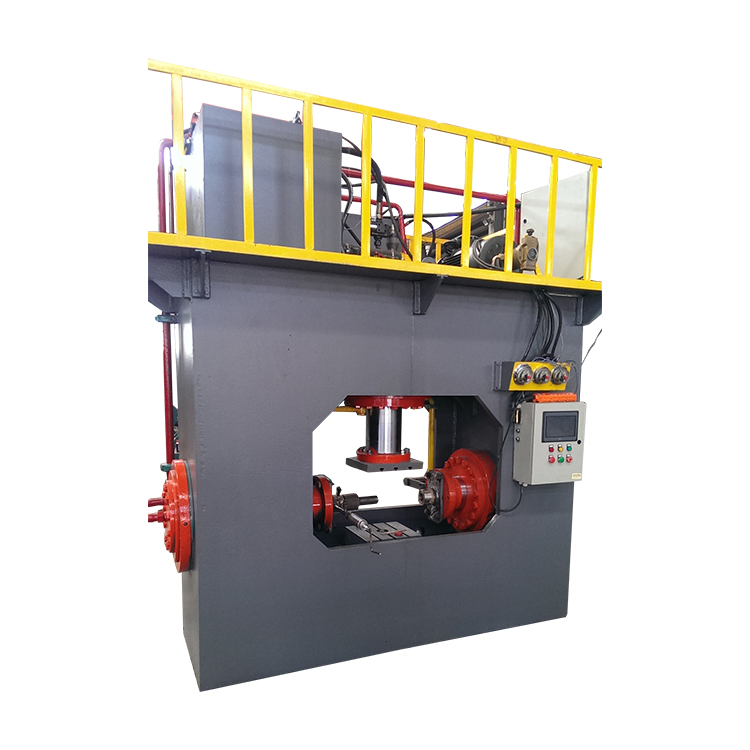
ternal high pressure tee machineIn
Mechanical parameters
|
Model |
1/2”—4” |
1”—6” |
2”—8” |
3”—10” |
4”—12” |
5”—16” |
8”—20” |
|
T wall thickness |
Sch40 |
||||||
|
Maximum pressure |
31.5MPa |
||||||
|
Pressure of work |
25 MPa |
||||||
|
In her work |
0—1000mm/min |
||||||
|
Returns the speed |
1500—2000mm/min |
||||||
|
Side of the cylinder bore |
360mm*2 |
450mm*2 |
550mm*2 |
650mm*2 |
750mm*2 |
850mm*2 |
950mm*2 |
|
The side cylinder stroke |
300mm |
350mm |
400mm |
450mm |
500mm |
550mm |
600mm |
|
The side cylinder tonnage |
250T*2 |
400T*2 |
600T*2 |
850T*2 |
1100T*2 |
1400T*2 |
1600T*2 |
|
Master cylinder bore |
400mm |
500mm |
600mm |
700mm |
800mm |
900mm |
1000mm |
|
Master cylinder stroke |
350mm |
400mm |
500mm |
600mm |
700mm |
800mm |
900mm |
|
Master cylinder tonnage |
315T |
500T*2 |
700T |
1000T |
1200T |
1600T |
2000T |
|
The motor power |
50w |
55kw |
65kw |
75kw |
100kw |
120kw |
170kw |
Mechanical video
Equipment details
ternal high pressure tee machineIn
Internal high pressure tee machine is used for carbon steel, stainless steel pipe into a special hydraulic machine, suitable for all kinds of specifications of tee pipe fitting joint extrusion molding change the position of the cylinder, can be processed and manufactured 90 degrees, 135 degrees and other angles of tee pipe joint.In high pressure tee machine has the independence actuating unit and the electrical system, PLC programmable controller, which can realize point, manual, semiautomatic and fully automatic four kinds of operation mode, automatic function with cavity filling, increase, pressure release part adopts the advanced hydraulic control technology, increased the safety and reliability, the high-voltage tee machine rational layout, use convenient maintenance, reliable operation, high production efficiency, product quality is good.
Operation steps of internal high pressure three-way machine: first place the fixing plate inside the first cavity, then put one end of the pipe fitting inside the groove of the fixing plate, at this time the outer wall of the pipe fitting and the upper end of the belt contact.Then the driving belt wheel is turned to turn the belt and the driven belt wheel.The static friction force between the outer wall of the pipe fitting and the belt and the operator's thrust force are used to push the pipe fitting placed on the belt to the fixed plate along the opening direction of the groove.After the pipe fitting is completely placed on the fixed plate, start the hydraulic cylinder to extend out so as to push the fixed plate and the pipe fitting placed on the fixed plate upward, and then weld the pipe fitting.The hydraulic cylinder is used to control the lifting height of the fixed plate, and the belt, active belt wheel and driven belt wheel are used to drive the pipe fitting to be placed on the fixed plate, which facilitates the feeding of the large-diameter pipe fitting and reduces the labor intensity of the operator.
- About us ABOUT US Company culture Production ability Service Process Service philosophy
- Device list ELBOW MACHINE PIPE BENDING MACHINE EXPANDING MACHIEN TEE MACHINE BEVELING MACHINE PRESS MACHINE MOULDS
- Video Center ELBOW MACHINE PIPE BENDING MACHINE PIPE EXPANDING MACHINE TEE MACHINE VIDEO BEVELING MACHINE PRESS MACHINE MOULDS VIDEO
- News Center Company news Business news
- Contact us Contact us Web site map
-
