Chinese | English
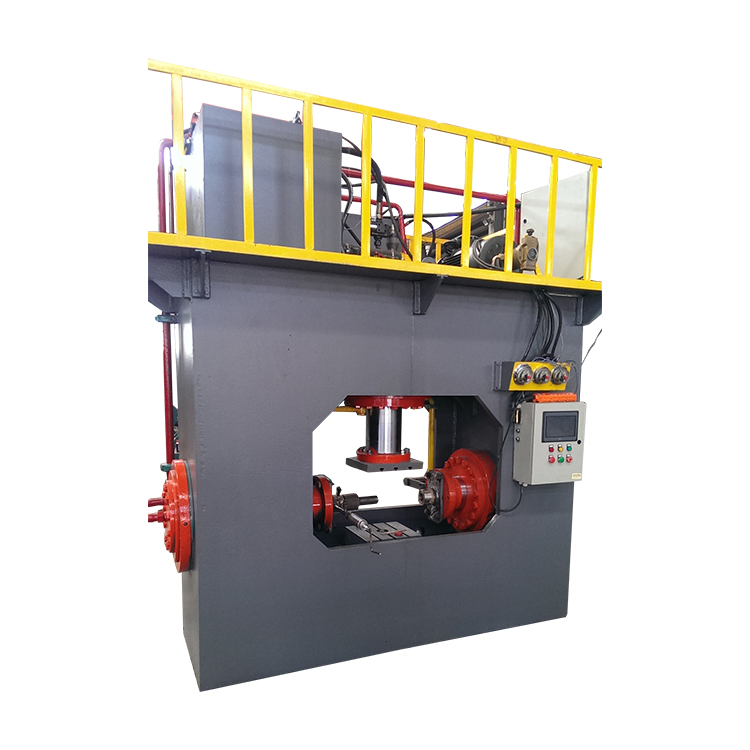
Cold drawing tee machine
Mechanical parameters
|
Model |
1/2”—4” |
1”—6” |
2”—8” |
3”—10” |
4”—12” |
5”—16” |
8”—20” |
|
T wall thickness |
Sch40 |
||||||
|
Maximum pressure |
31.5MPa |
||||||
|
Pressure of work |
25 MPa |
||||||
|
In her work |
0—1000mm/min |
||||||
|
Returns the speed |
1500—2000mm/min |
||||||
|
Side of the cylinder bore |
360mm*2 |
450mm*2 |
550mm*2 |
650mm*2 |
750mm*2 |
850mm*2 |
950mm*2 |
|
The side cylinder stroke |
300mm |
350mm |
400mm |
450mm |
500mm |
550mm |
600mm |
|
The side cylinder tonnage |
250T*2 |
400T*2 |
600T*2 |
850T*2 |
1100T*2 |
1400T*2 |
1600T*2 |
|
Master cylinder bore |
400mm |
500mm |
600mm |
700mm |
800mm |
900mm |
1000mm |
|
Master cylinder stroke |
350mm |
400mm |
500mm |
600mm |
700mm |
800mm |
900mm |
|
Master cylinder tonnage |
315T |
500T*2 |
700T |
1000T |
1200T |
1600T |
2000T |
|
The motor power |
50w |
55kw |
65kw |
75kw |
100kw |
120kw |
170kw |
Mechanical video
Equipment details
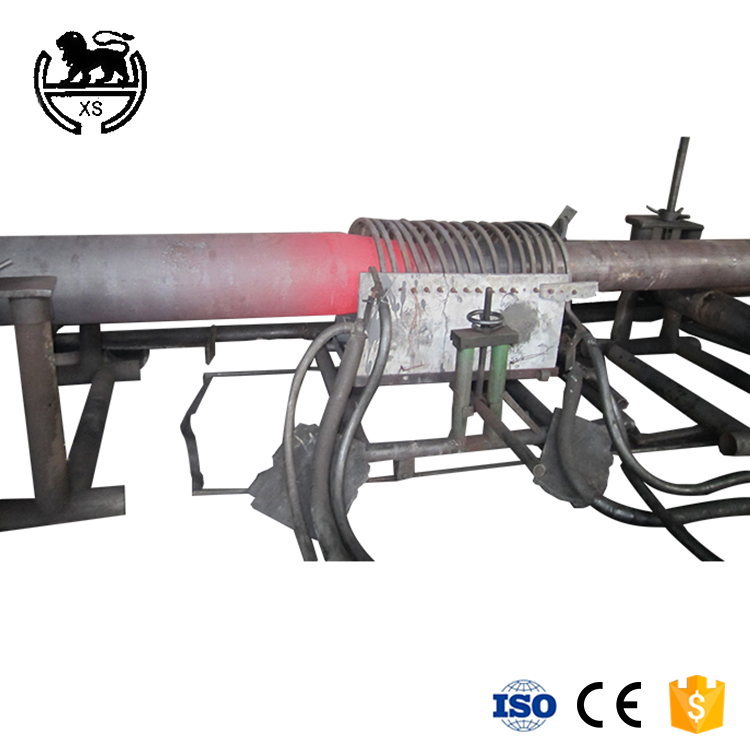
Production process of cold-drawing tee: cold-drawing tee tube device is a special equipment for cold-drawing tee tube fitting, including metal bar, top pressure device, commutator, support, etc.;When the jacks and metal bars are pushed out, the cold-drawn tee blank formed by the pipe wall material is turned out naturally.Then the pipe segment of a certain length corresponding to the specification is welded on the blank of cold-drawn tee formed by ejecting to produce the final product.
Installation method of cold-drawing tee machine: firstly, hole is made on the steel pipe with a hole opener, and then the mechanical tee is stuck into the hole. The hole is sealed by the sealing ring along the pipe wall.Mechanical three - way wire connection and groove type two.When the mechanical tee is connected, the clearance between the mechanical tee and the hole should be checked. All parts should be even, and then the fastening should be in place.Mechanical tee hole spacing shall not be less than 1m.
The hydraulic expansion of three - way is a forming process of the branch pipe through the axial compensation expansion of metal materials.Namely the hot three - way cold squeeze technology.
(1) special hydraulic press is used to inject liquid into the billet with the same diameter as the tee.(2) two horizontal side cylinders of the hydraulic press are used to simultaneously press the tube billet in the middle movement. The volume of the tube billet becomes smaller after extrusion. The liquid in the tube billet increases with the decrease of the tube billet volume.The thickness of main pipe and shoulder wall of tee has increased.
- About us ABOUT US Company culture Production ability Service Process Service philosophy
- Device list ELBOW MACHINE PIPE BENDING MACHINE EXPANDING MACHIEN TEE MACHINE BEVELING MACHINE PRESS MACHINE MOULDS
- Video Center ELBOW MACHINE PIPE BENDING MACHINE PIPE EXPANDING MACHINE TEE MACHINE VIDEO BEVELING MACHINE PRESS MACHINE MOULDS VIDEO
- News Center Company news Business news
- Contact us Contact us Web site map
-
