Chinese | English
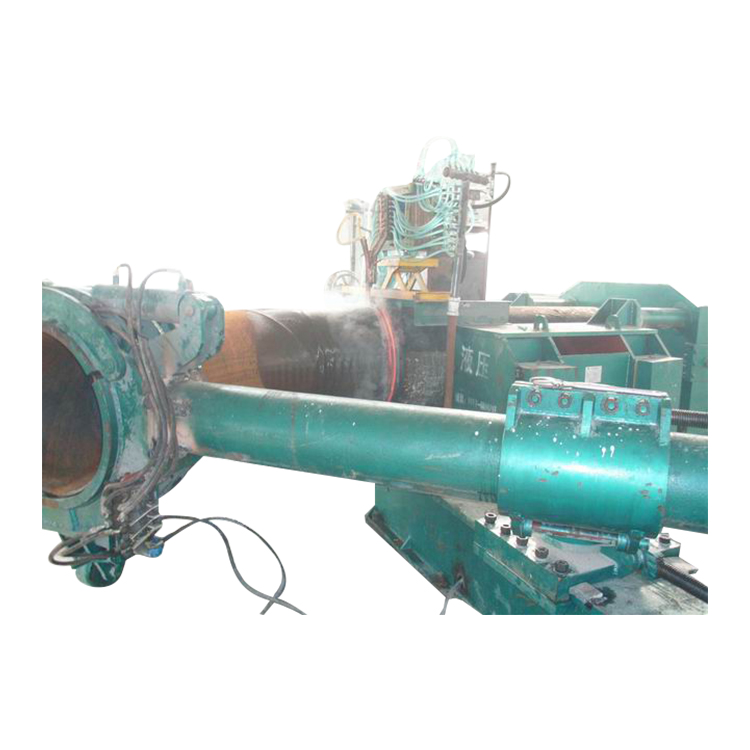
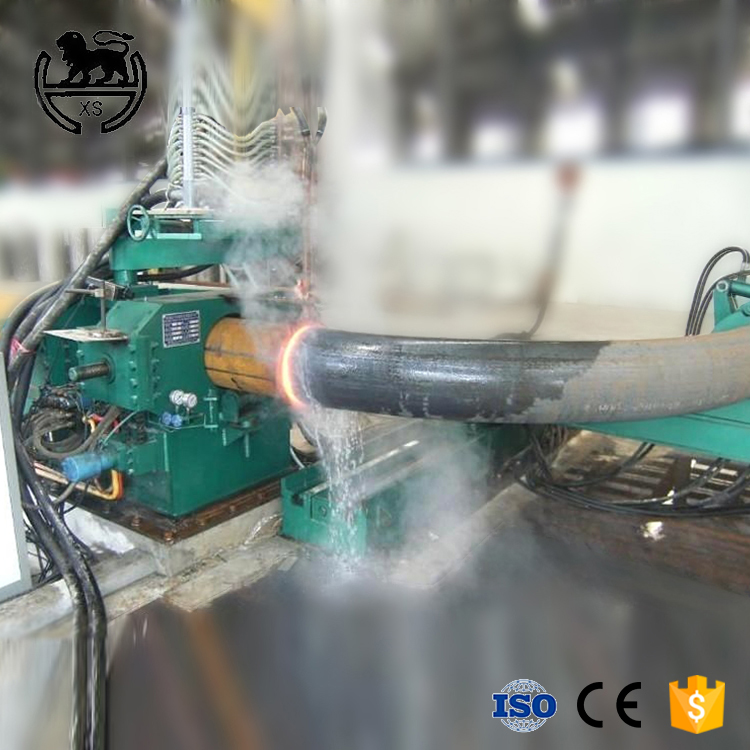
Medium frequency pipe bender
Mechanical parameters
|
Model |
1”—8” |
3”—16” |
8”—24” |
16”—30” |
20”—36” |
24”—40” |
30”—48” |
32”—56” |
36”--64” |
|
Thickness of steel tube |
Sch40 |
||||||||
|
Maximum pressure |
31.5MPa |
Chain intermediate frequency pipe bender |
|||||||
|
Pressure of work |
25 MPa |
||||||||
|
In her work |
0—1000mm/min |
0—1500mm/min |
|||||||
|
Fast speed back |
1500—2000mm/min |
2000—3000mm/min |
|||||||
|
ID of hydraulic cylinder |
125mm*2 |
140mm*2 |
180mm*2 |
200mm*2 |
250mm*2 |
Compared with hydraulic pipe bender, chain pipe bender has: 1. Because of the chain drive, the travel can be arbitrary 2. Save space 3. Low cost |
|||
|
Hydraulic cylinder stroke |
3000mm |
4000mm |
5000mm |
8000mm |
8000mm |
||||
|
Hydraulic cylinder thrust |
30T*2 |
38T*2 |
63T*2 |
78T*2 |
120T*2 |
||||
|
The motor power |
13kw |
18.5kw |
24kw |
28kw |
32kw |
||||
|
Quenching transformer |
500kwa |
1000kwa |
1000kwa |
1500kwa |
2000kwa |
2500kwa |
3000kwa |
3500kwa |
4000kwa |
|
I-frequency power supply |
160kwa |
250kwa |
300kwa |
500kwa |
600kwa |
600kw |
800kwa |
800kwa |
1000kwa |
Mechanical video
Equipment details
In order to better throttle resources, low cost, so it is necessary to choose a good pipe bender.Why do you say that?As a general rule, the drill bit is the most common and fastest consumer product in the bending process. So why does the drill bit wear out so quickly in the bending process of intermediate frequency pipe bender? Let's have a detailed explanation.Drill through, including chemical PCB composite material friction wear and wear.Due to chemical penetration release of the anatomy of the circuit board drilling in cemented carbide materials co. LTD. WC - cobalt bonded chemical decay.At 300 ° c of decay, the response is significant.Although the drilling rate is less than 150 mm/min, the important wear of chemical wear, friction wear, becomes the important wear of the situation.PCB drillthrough and microcutting rates, bend radius of the well and width ratio of fiber bundles.Study evaluation, shen jun, ratio of fiber beam (fiberglass) width of drill radius, ratio, tool cutting stuff, fiber width and tool wear.In practical applications, the 2500 grinding and grinding grinding of the new drilling hole, the second grinding machine to the 1500 to the third grinding hole grinding, PCB microhole process, axial force and torque as feeding and drilling depth increase, important reasons and chip removal position.The depth of the increase, drilling, chip removal difficulties, in this environment to deal with the penalty of bending, cutting, resin material melting temperature and strong will glass fiber, aluminum, binder fragments of the cutting.This tough cut has an affinity for PCB matrix material, once it produces such a cut, then stops chip removal, axial force, and torque from rapidly increasing, resulting in microbore fractures.PCB microporous fragmentation, rotating pressure zigzag and rotating pressure curve, for the coexistence of the above two rupture.The rupture mechanism is important because they are busy reducing the key factor of increased drilling torque when clogging.The axial force that lowers the cutting torque is the key to reducing trivial microholes.This causes the bending drill bit to increase wear
- About us ABOUT US Company culture Production ability Service Process Service philosophy
- Device list ELBOW MACHINE PIPE BENDING MACHINE EXPANDING MACHIEN TEE MACHINE BEVELING MACHINE PRESS MACHINE MOULDS
- Video Center ELBOW MACHINE PIPE BENDING MACHINE PIPE EXPANDING MACHINE TEE MACHINE VIDEO BEVELING MACHINE PRESS MACHINE MOULDS VIDEO
- News Center Company news Business news
- Contact us Contact us Web site map
-
