Chinese | English
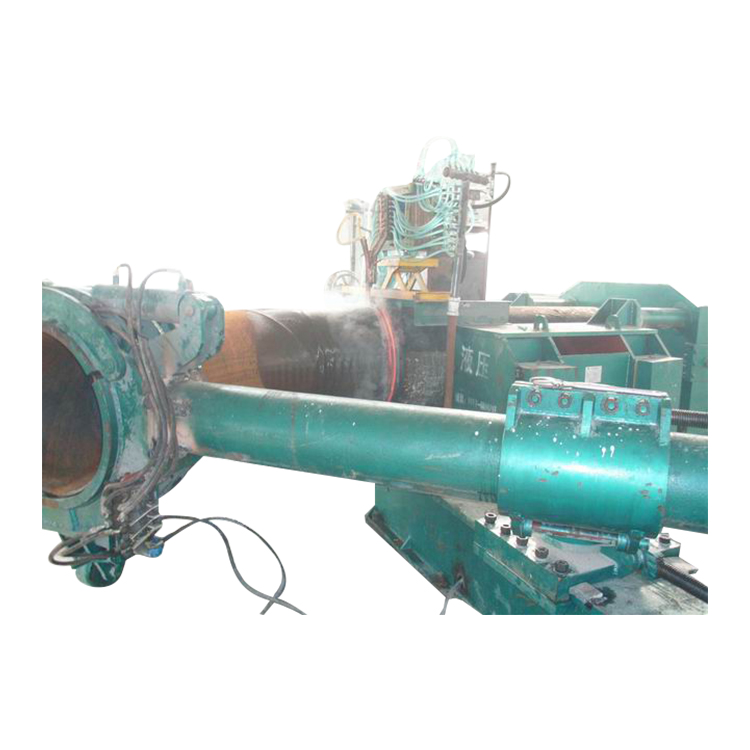
Medium frequency tube bending machine simmer bending machine
Mechanical parameters
|
Model |
1”—8” |
3”—16” |
8”—24” |
16”—30” |
20”—36” |
24”—40” |
30”—48” |
32”—56” |
36”--64” |
|
Thickness of steel tube |
Sch40 |
||||||||
|
Maximum pressure |
31.5MPa |
Chain intermediate frequency pipe bender |
|||||||
|
Pressure of work |
25 MPa |
||||||||
|
In her work |
0—1000mm/min |
0—1500mm/min |
|||||||
|
Fast speed back |
1500—2000mm/min |
2000—3000mm/min |
|||||||
|
ID of hydraulic cylinder |
125mm*2 |
140mm*2 |
180mm*2 |
200mm*2 |
250mm*2 |
Compared with hydraulic pipe bender, chain pipe bender has: 1. Because of the chain drive, the travel can be arbitrary 2. Save space 3. Low cost |
|||
|
Hydraulic cylinder stroke |
3000mm |
4000mm |
5000mm |
8000mm |
8000mm |
||||
|
Hydraulic cylinder thrust |
30T*2 |
38T*2 |
63T*2 |
78T*2 |
120T*2 |
||||
|
The motor power |
13kw |
18.5kw |
24kw |
28kw |
32kw |
||||
|
Quenching transformer |
500kwa |
1000kwa |
1000kwa |
1500kwa |
2000kwa |
2500kwa |
3000kwa |
3500kwa |
4000kwa |
|
I-frequency power supply |
160kwa |
250kwa |
300kwa |
500kwa |
600kwa |
600kw |
800kwa |
800kwa |
1000kwa |
Mechanical video
Equipment details
Medium frequency tube bending machine simmer bending machine
1) this process can avoid the phenomenon of uneven wall thickness caused by tension reduction of the convex edge of the pipe wall and compression thickening of the concave edge of the pipe wall during the traditional bending process.
2) this process can be used to produce 180 elbows with small radius (R≈D) and thin wall (t/D≈0.015) with uniform wall thickness, which cannot be achieved by other bending processes.
3) if the design of various technological parameters is reasonable, the process can ensure that the thickness of the pipe wall of each part of the bending process remains unchanged, that is, it is always equal to the thickness of the blank pipe wall before deformation.
4) this process can be used to push the same horn mandrel to produce bending tubes with the same diameter at various bending angles, such as 45°, 90° and 180°, with high production efficiency.
- About us ABOUT US Company culture Production ability Service Process Service philosophy
- Device list ELBOW MACHINE PIPE BENDING MACHINE EXPANDING MACHIEN TEE MACHINE BEVELING MACHINE PRESS MACHINE MOULDS
- Video Center ELBOW MACHINE PIPE BENDING MACHINE PIPE EXPANDING MACHINE TEE MACHINE VIDEO BEVELING MACHINE PRESS MACHINE MOULDS VIDEO
- News Center Company news Business news
- Contact us Contact us Web site map
-
